Home / What We Do / Apparel
Apparel
Owned by one team, from cut to pack.Apparel is MTM’s flagship — converting our own yarn and fabric into finished garments through five in-house functions, with no subcontractor touching your product at any stage.
Home / What We Do / Apparel
Owned by one team, from cut to pack.Apparel is MTM’s flagship — converting our own yarn and fabric into finished garments through five in-house functions, with no subcontractor touching your product at any stage.
Because cutting, stitching, printing, embroidery and garment processing all sit inside MTM, one team owns cost, quality, lead time and finish on every garment that leaves the floor.
Automatic high-ply cutting on Gerber Paragon and Orox systems handles bulk programmes; manual tables handle stripe-matched and jacquard styles where panel alignment needs a human hand. Gerber AccuMark CAD and Shape Shifter marker optimisation select the most fabric-efficient cut plan for each order.
Three factories in Faisalabad, fully compliant with international social, ethical, environmental and quality requirements. A dedicated industrial-engineering function balances and sizes every line before production starts — which is why lead times stay predictable at every order volume.
Four capabilities in-house: digital (unlimited colour, no setup cost, ideal for sampling and short runs), screen (automatic for bulk, manual for specialty placement), heat-transfer for polyester sportswear and team-kit personalisation, and embossed relief effects.
Multi-head computerised Barudan machines from Japan perform direct, appliqué, puffy (3D) and label embroidery — from clean logos to the high-stitch-count motifs premium polo and licensed-sportswear programmes demand.
Garment dyeing across reactive, direct, pigment, sulphur and discharge chemistry, and washing across enzyme, acid, sand, silicone, vintage and spray treatments — the lived-in and luxury-soft finishes that define contemporary fashion.
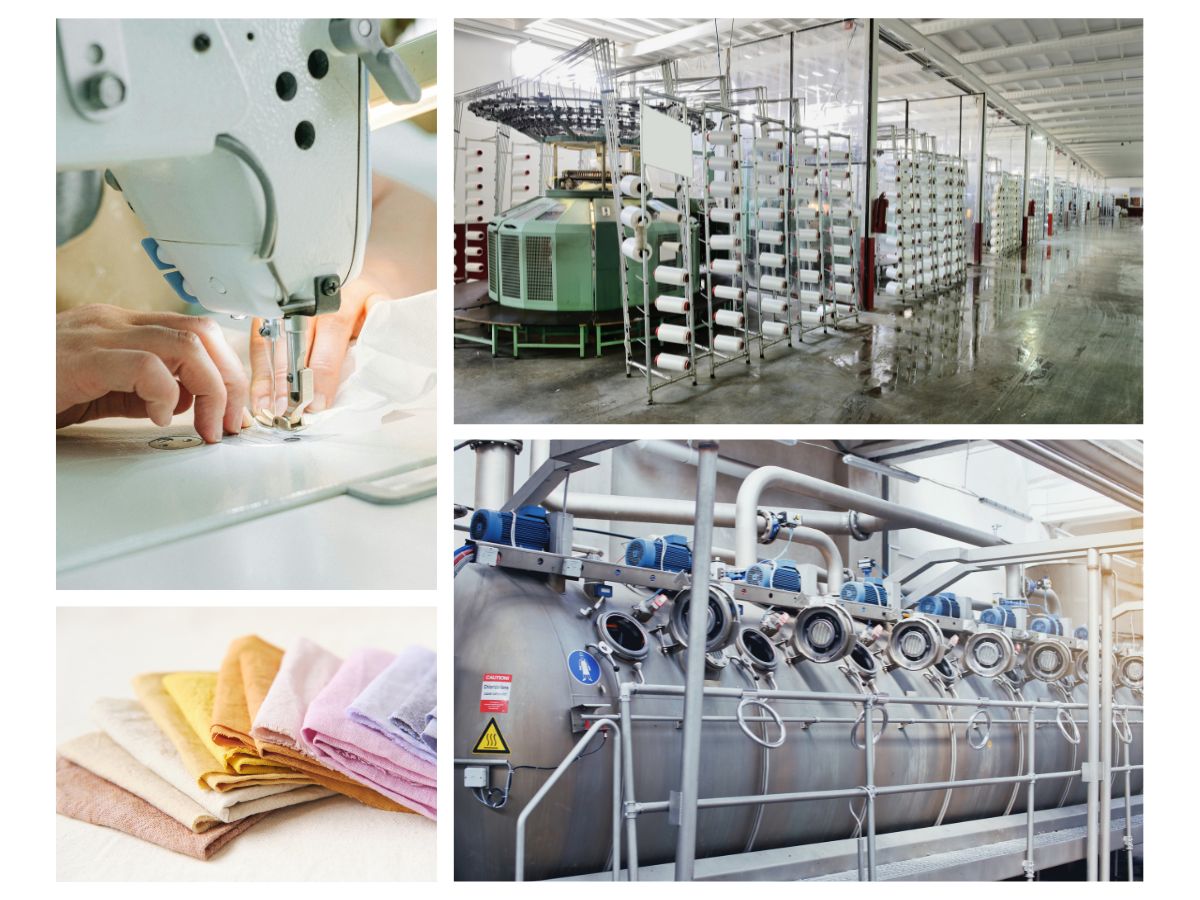
One accountable team across every product type we build — converting our own yarn and fabric, so a decision taken upstream is already understood downstream.


One team will come back to you on costing, capacity and lead time — with the fabric and yarn behind the garment already inside the same company.